
Copper Busbars for Energy-Storage Cabinets, Progressive-Die Formed
Table of Contents
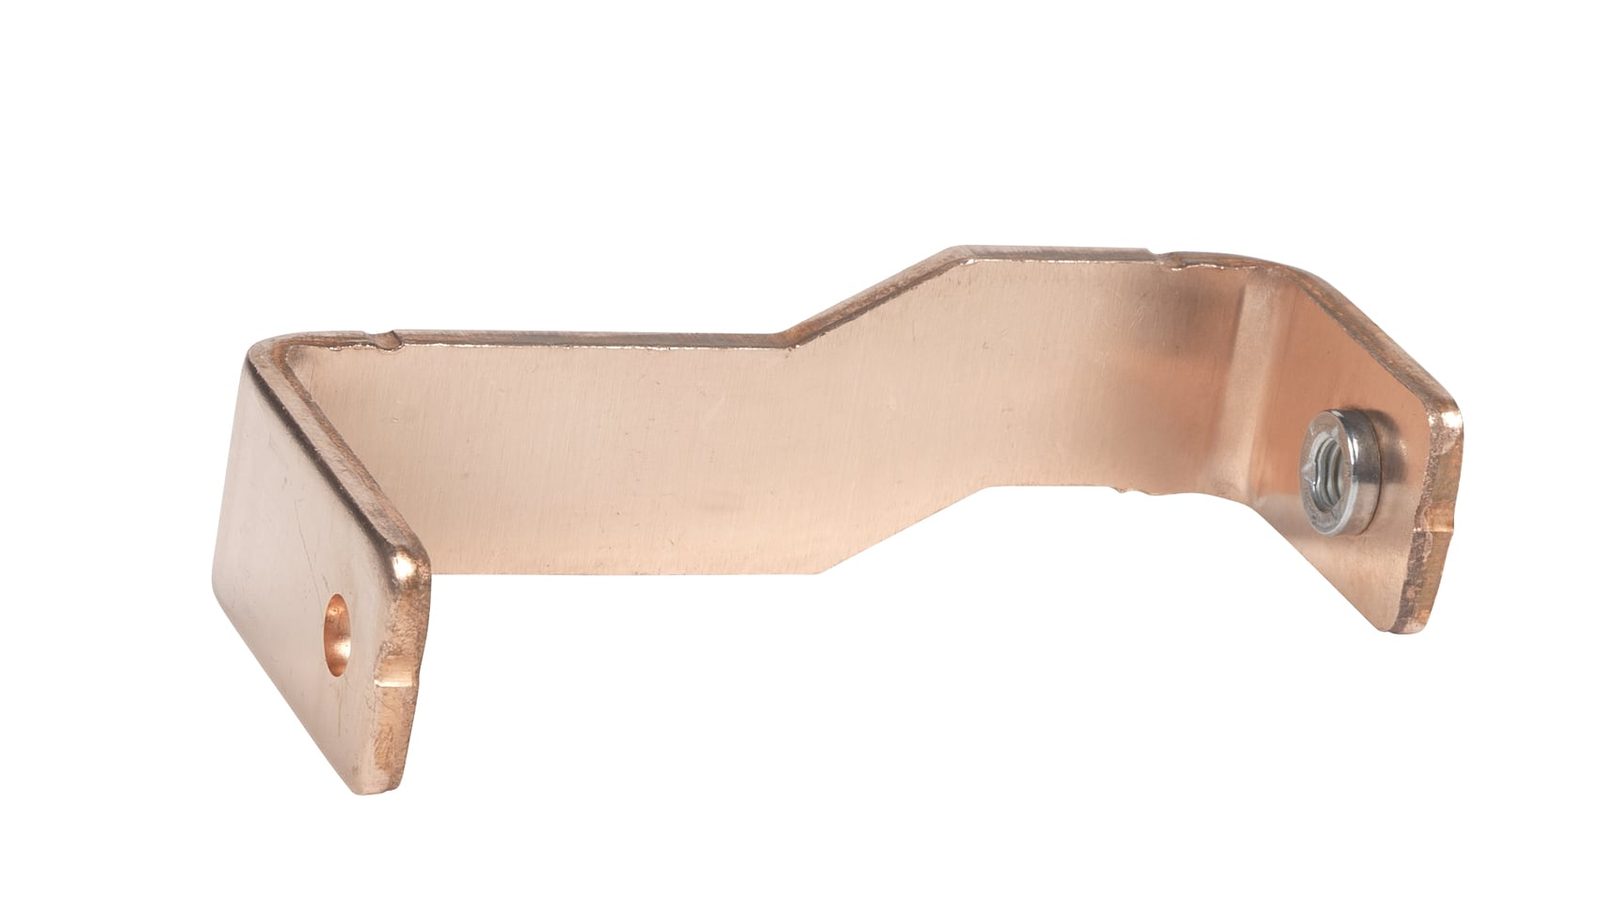
A manufacturer of energy-storage and EV-charging cabinets came to us with a busbar problem: parts were cut and formed one operation at a time, so bend angles drifted across the batch. Assemblers were straightening busbars at the workstation before mounting, and the rectifier shelf build schedule kept slipping.
We moved the part onto a progressive die. Blanking, corner cut, and the two bend stations run in one tool, so each press stroke ejects a finished busbar. Tooling was designed, machined, assembled, and T1-trialled in our own tool room — three die revisions during DFM took days, not the weeks a purchased tool would have meant.
Outcome
- Bend angle held inside ±0.5°, overall dimensions within ±0.005 mm
- Daily output absorbed into a line rated 500,000+ pcs/day; no manual rework reported at the customer's shelf-assembly station
- Tooling lead time 2–5 weeks; engineering feedback on drawings
Specifications
material C1100 copper · thickness within our 0.05–3.0 mm range · presses 25–110 T · up to 300 SPM · 100% in-house tooling · inspection on 2D vision projectors (±0.005 mm)
Industries Served
See how we stamp for E-Mobility / Electric VehiclesMore Case Studies
NEXT STEP
Have a Similar Part?
Send your drawing and annual volume — our engineers return a DFM review and quote for parts like this one.
Written by
Ray ChanExport Brand Manager. Ray helps global engineers and buyers source precision metal stamping parts and assemblies.