
Medical Metal Stampings — Precision in Medical Alloys
Medical metal stamping for sensor components, surgical instrument parts and device contacts - stamped in SUS301/304/316L stainless and C17200 beryllium copper at ±0.005 mm positioning on 21 high-speed presses, with material certificates and lot traceability on every shipment.
NDA ProtectedFast Quote ResponseSTEP, IGES, X_T, DWG
Trusted Tier-1 & OEM Standards:
CHALLENGES WE SOLVE
Medical Stamping Challenges & Our Solutions
Four recurring medical failure modes seen in incoming RFQs — and how each is prevented on our line.
01
Medical device components
The Challenge
Tolerance stack-up across progressive stages drifts critical features out of spec lot by lot.
Our Solution
Held with 0.005 mm positioning precision and 100% dimensional inspection before packing.
02
Sensor parts
The Challenge
Micro-shift under vibration and thermal cycling puts sensor alignment out of tolerance.
Our Solution
Vibration-critical positions verified on optical measurement with lot-level records.
03
Surgical and orthopedic instrument components
The Challenge
High-speed press wear shifts positioning precision before the first inspection catches it.
Our Solution
Scheduled die maintenance and in-process checks catch drift between lots, not after.
04
Implantable device parts
The Challenge
Spring-back on high-strength alloys pulls formed features away from the drawing.
Our Solution
Form spring-back characterized at FAI and compensated in the die before production.
Need Medical Stampings That Meet Spec?
Send your drawing — engineering runs a free DFM review and pricing follows the review.
ENGINEERING CAPABILITIES
Medical Stamping Specifications & Equipment
Part Specifications
| Specification Parameter | Automotive & EV Standard | High-Precision Custom |
|---|---|---|
| Part Thickness | 0.10 mm – 3.0 mm | Per drawing |
| Standard Tolerance | ±0.025 mm (±0.001 in) | Tighter on critical features |
| Positioning Precision | 0.005 mm | — |
| Press Capacity | 25–110 tons (21 presses) | — |
Equipment
Stamping Presses
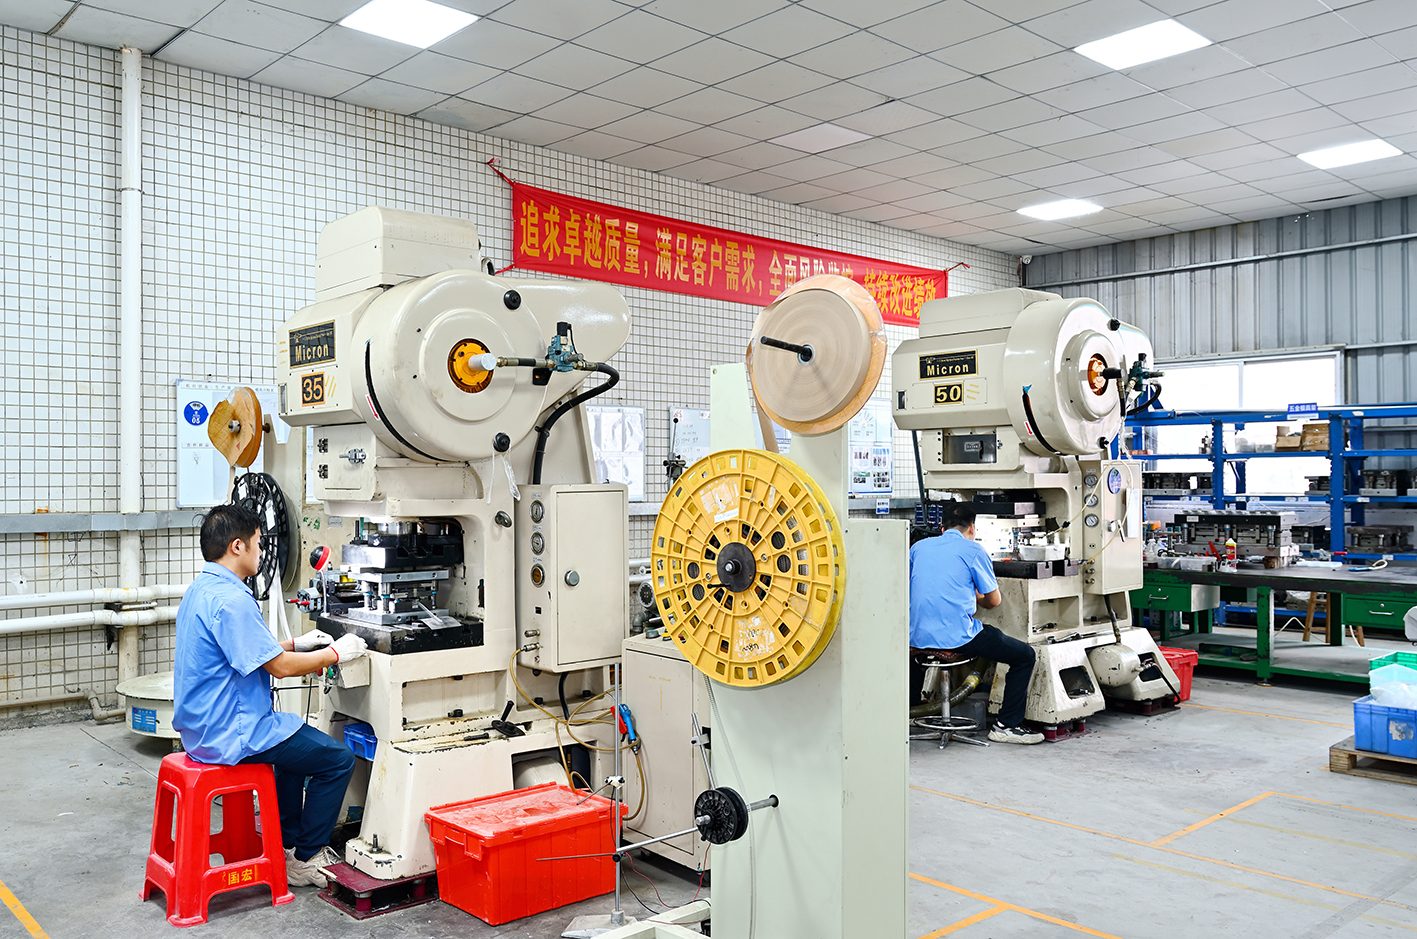
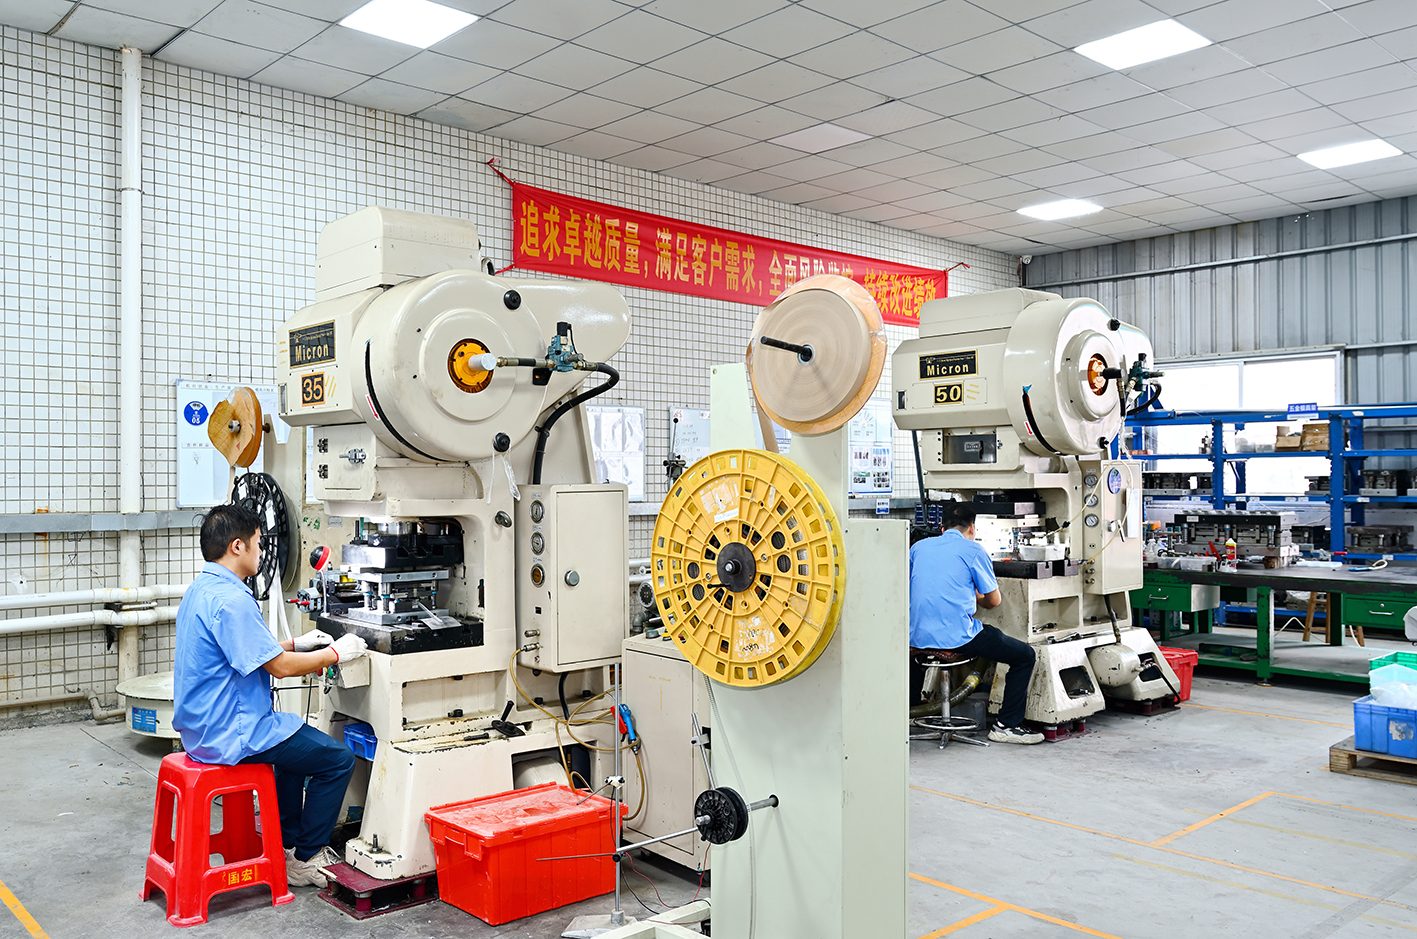
21 presses, 25–110T — up to 300 SPM with 0.005 mm positioning on the high-speed line.
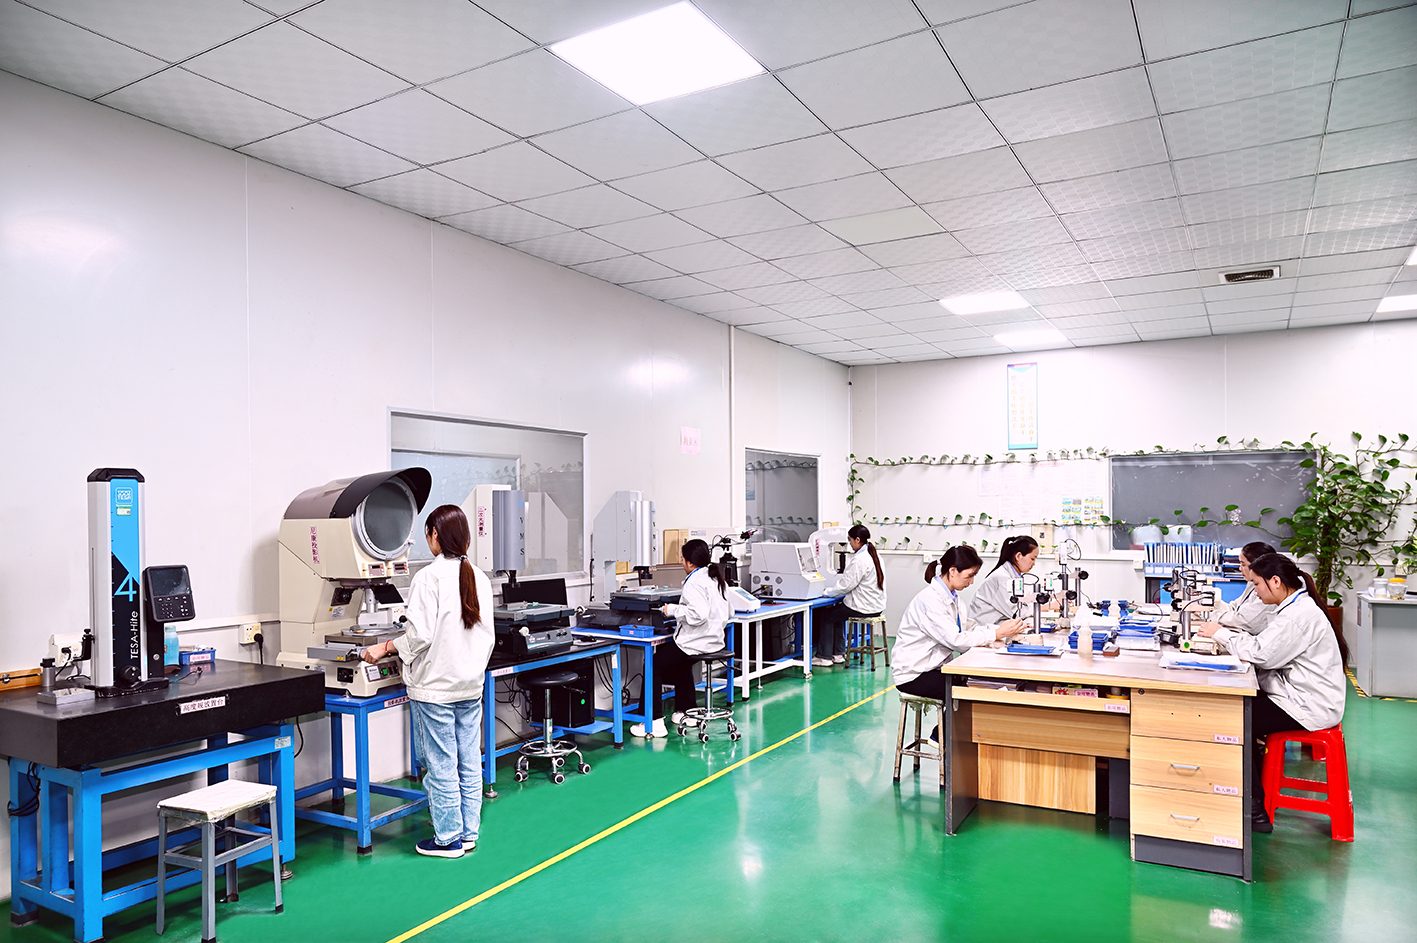
In-House Quality Lab
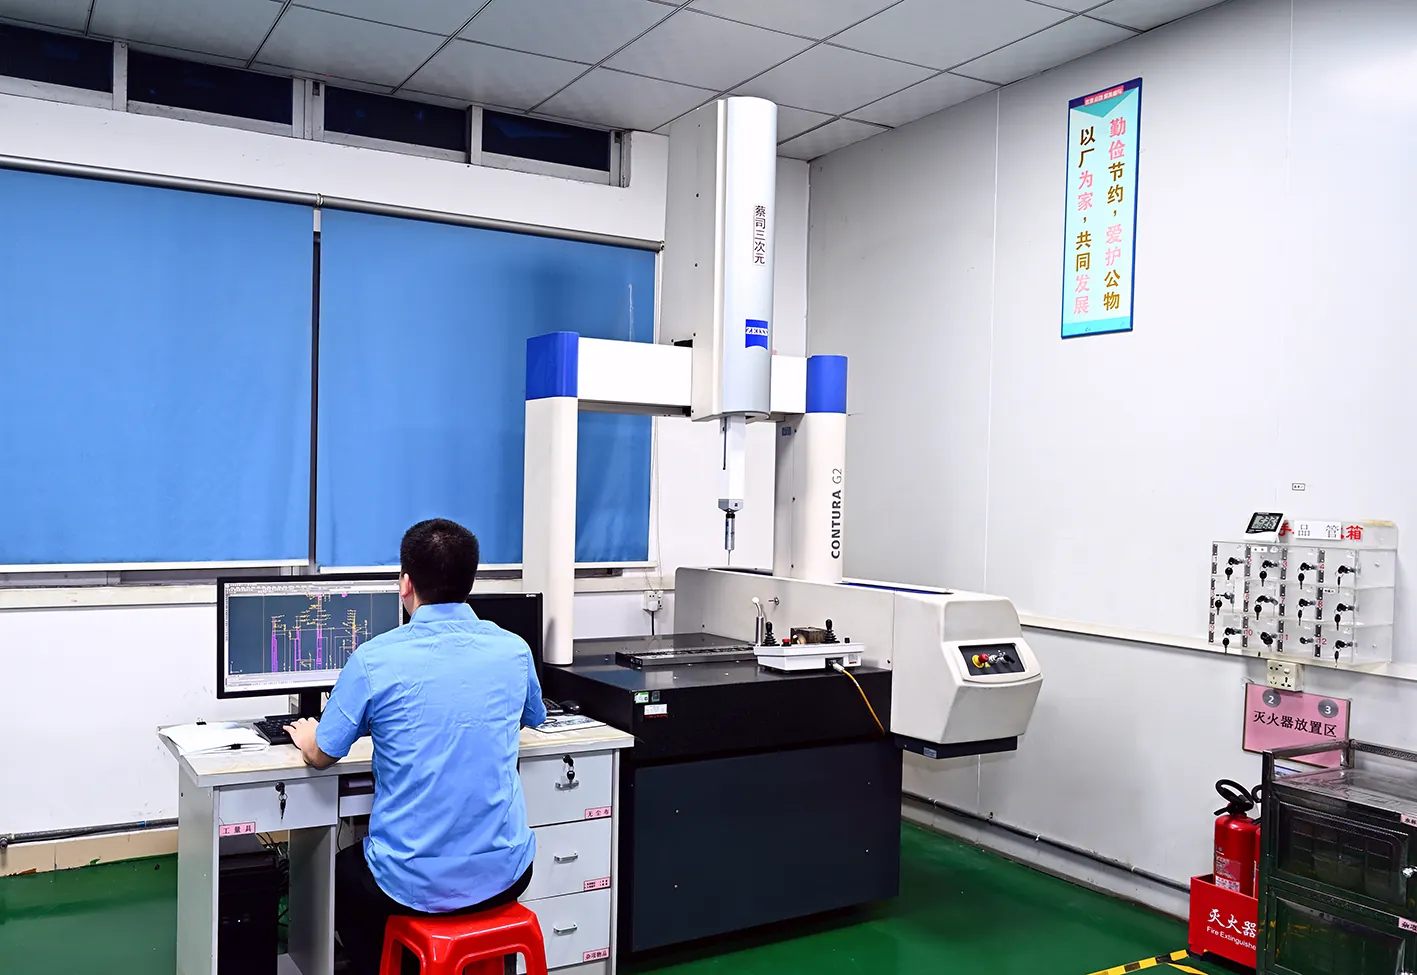
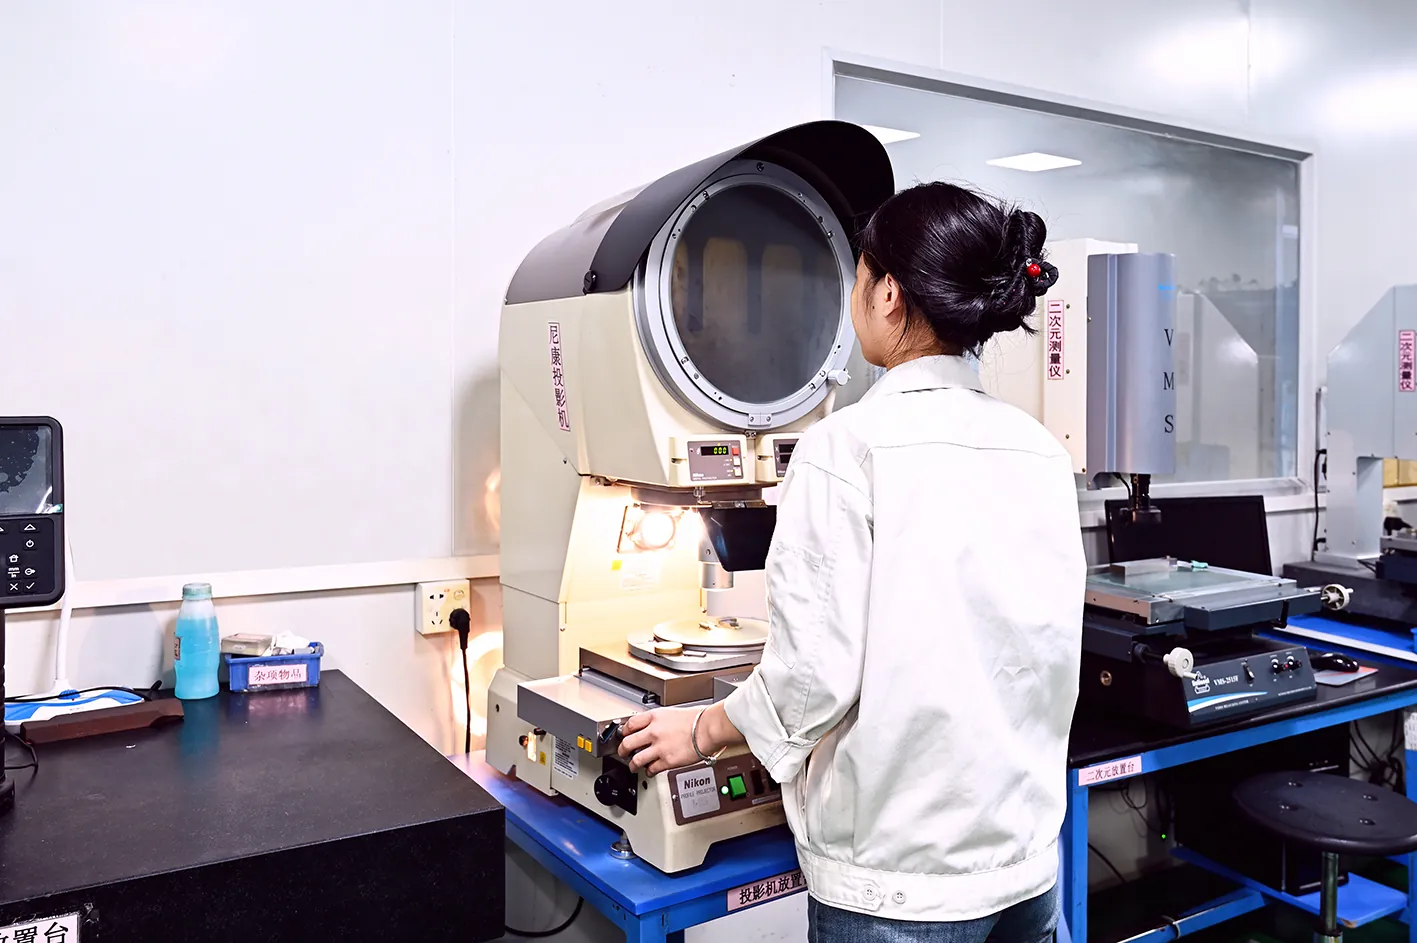
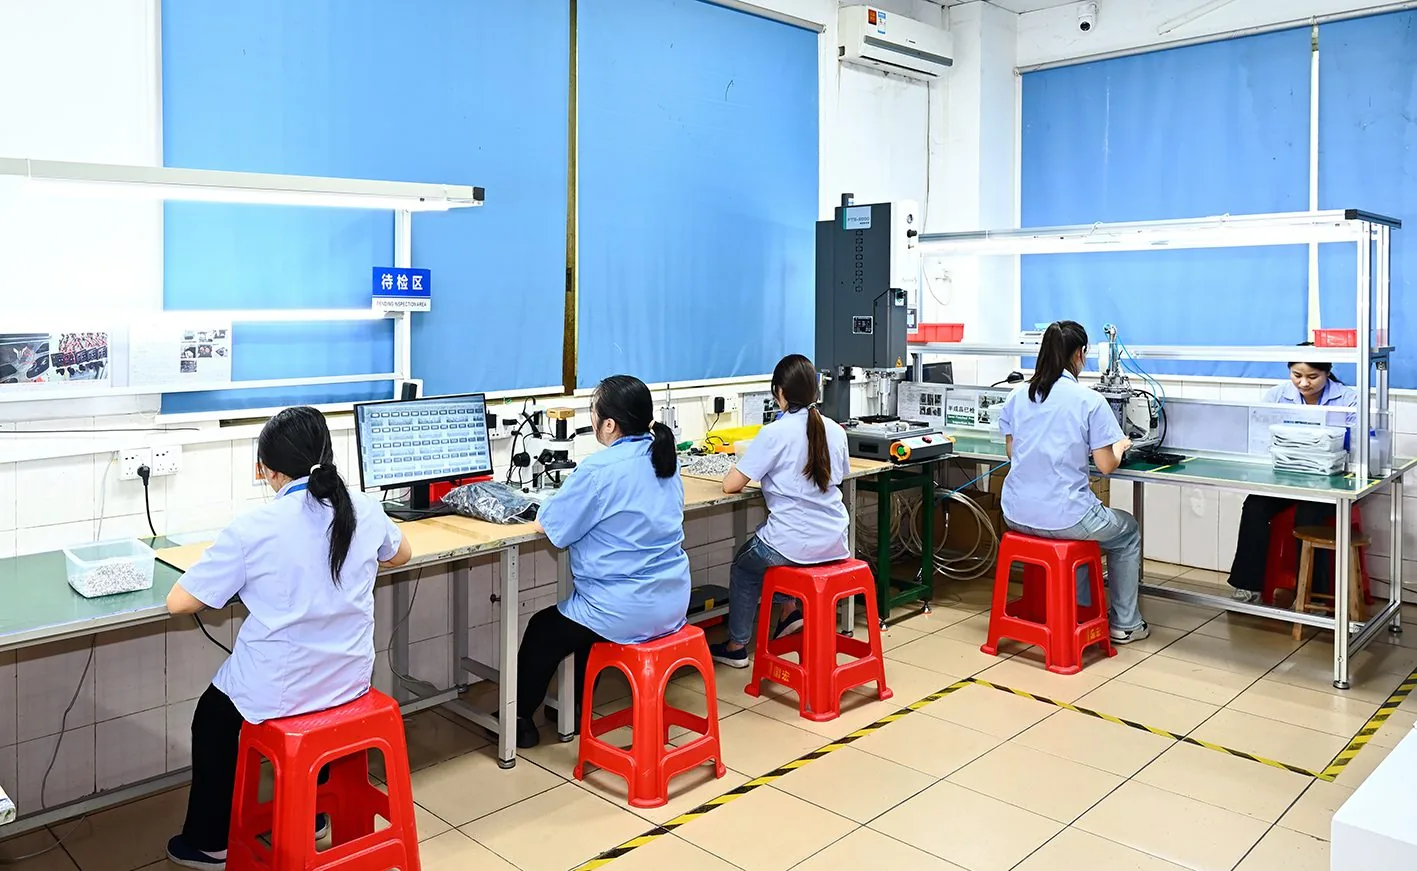
CMM and optical measurement verify critical features on every lot.
In-House Tool Room
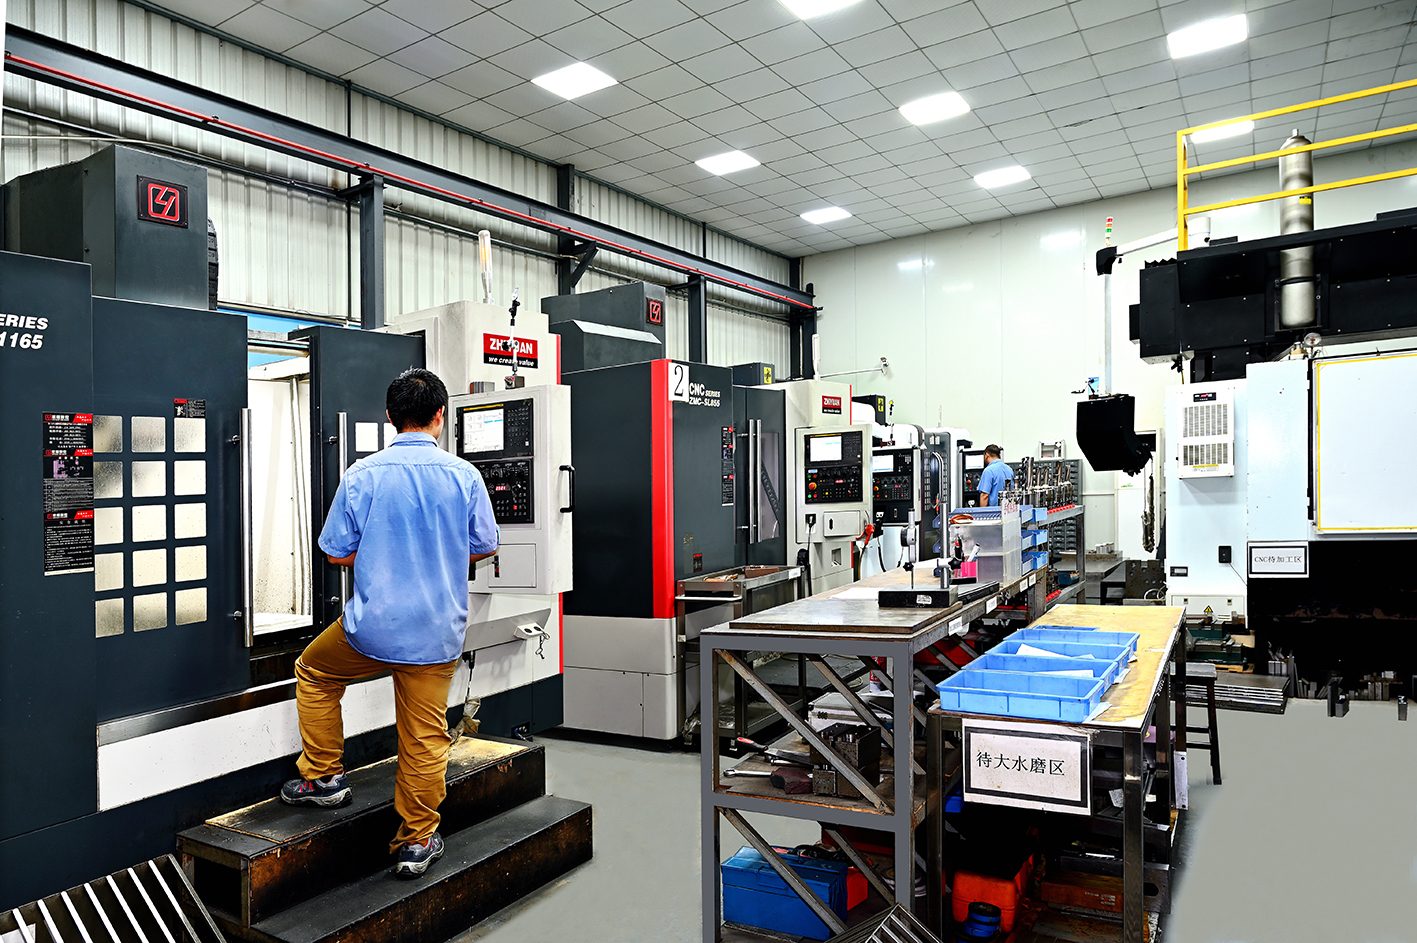
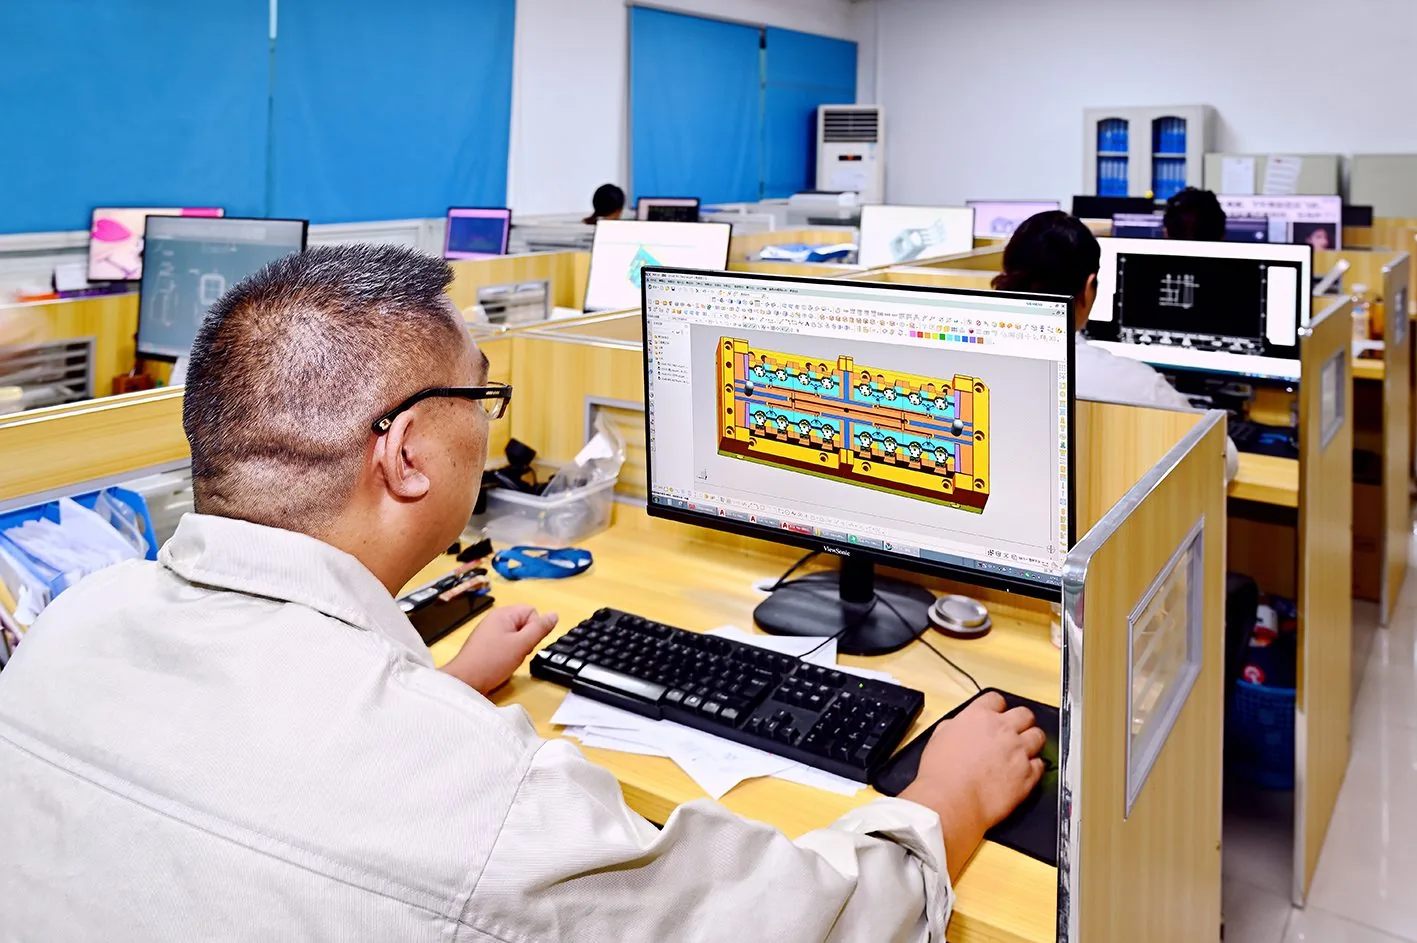
Wire EDM, CNC machining and optical profile grinding keep die design and build in one loop.
Reel-to-Reel Plating
Selective gold (2-8 µm), tin and zinc (5-12 µm) plating through approved partner lines for corrosion and conductivity.
APPLICATION & INDUSTRY SOLUTIONS
Metal Stampings for Medical
Medical device components
Stamped components for medical devices - validated processes, material certifications and full batch traceability on every lot.
Sensor parts
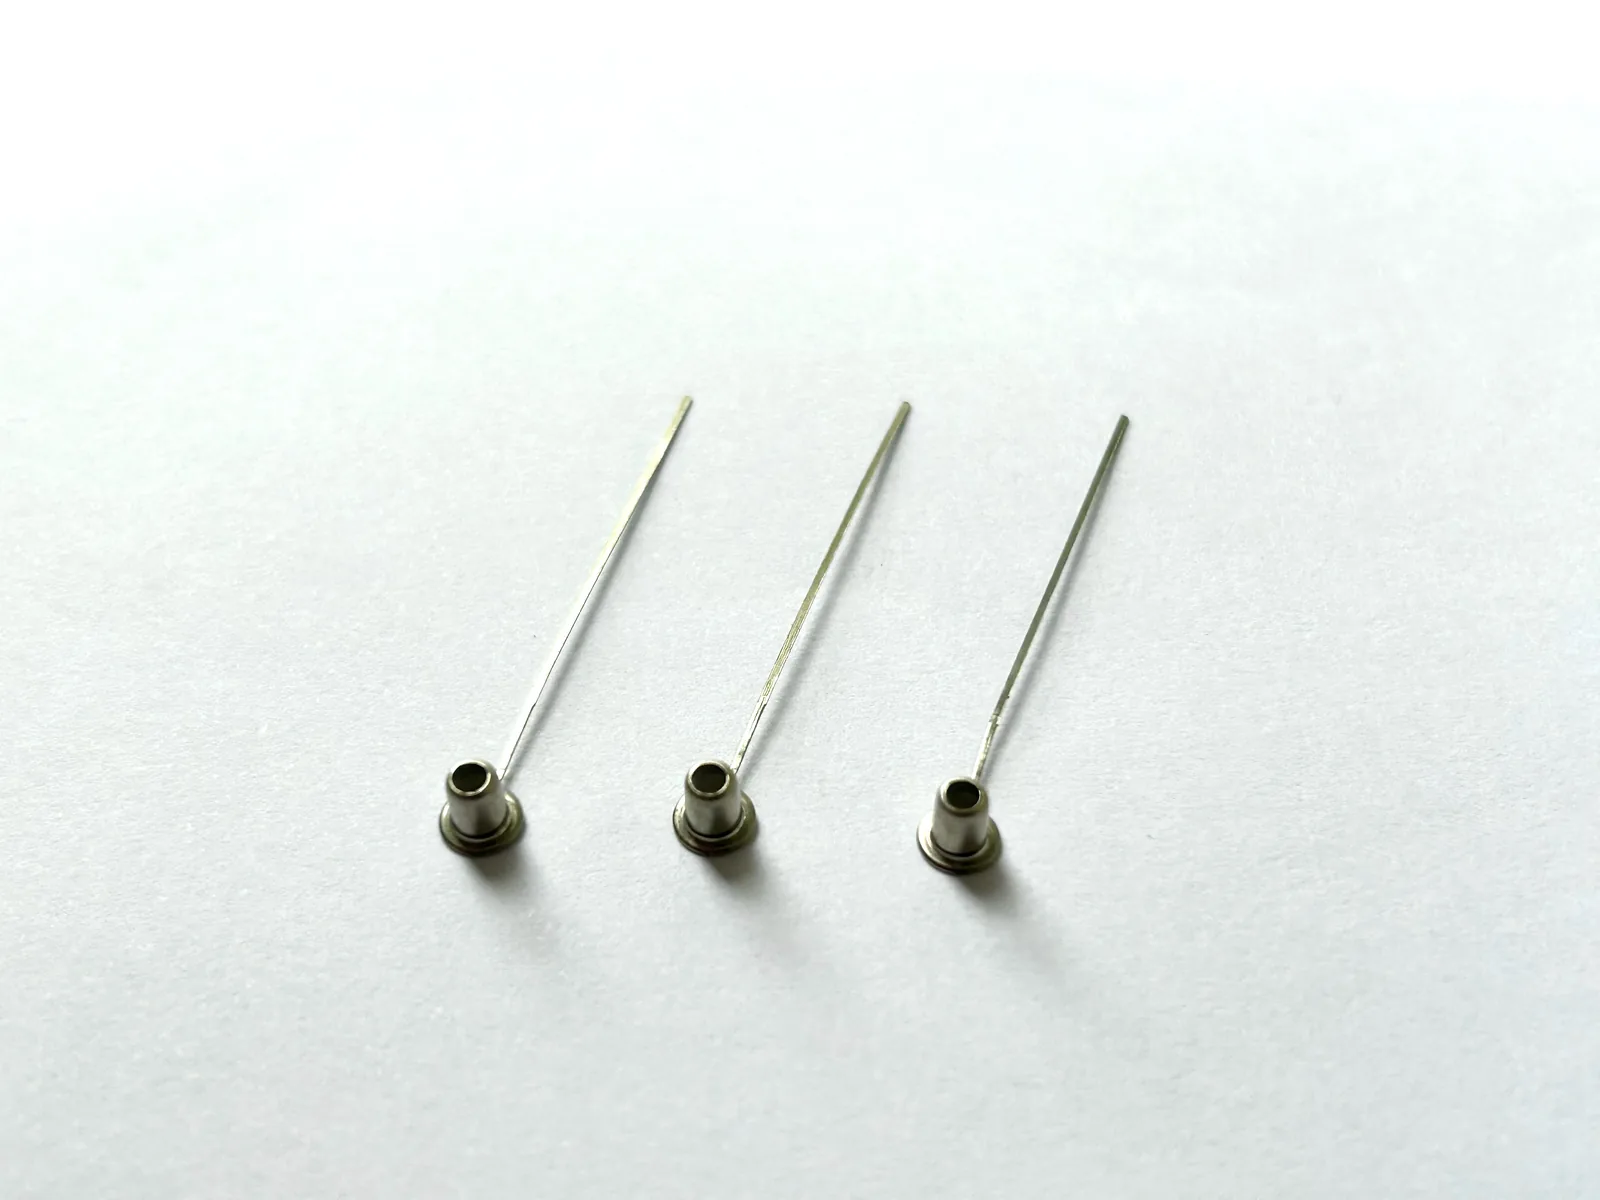
Precision stamped sensor components for medical monitoring equipment - tight tolerances and clean, burr-free surfaces.
Surgical and orthopedic instrument components
Stamped components for surgical instruments and orthopedic power tools - corrosion-resistant stainless steel with documented process controls.
Implantable device parts
Stamped parts for implantable device programs - biocompatible materials with strict traceability and validated processes.
Medical stamping
Precision Metal Stamping for Medical Devices
Medical device stamping demands precision, cleanliness and full traceability. ISTAMPING provides precision metal stamping for medical devices with validated processes, material certifications and batch traceability - from sensor components to surgical instrument parts.
- Validated processes and full batch traceability
- Material certifications with documented process controls
- Clean, burr-free precision for sensitive applications
- Dedicated production controls for medical programs
Medical stamping
Medical Device Progressive Stamping at High Volume
For the device parts we run — instrument hinges and jaw tips, contact springs, sensor diaphragms and lead-frame style terminals — the die, not the press count, sets the pace: progressive tooling with in-die sensing holds one station's misfeed from scrapping a coil. First-article reports, in-process dimensional checks and per-lot material certificates travel with each reel, so your incoming inspection and design-history-file paperwork pull from the same records we generated on the floor.
- High-speed progressive dies for medical device volumes
- In-house tooling designed for consistent, repeatable output
- Documented quality on every lot - the control medical demands
- Prototype to high-volume production support
Medical stamping
Stainless, Beryllium Copper and Burrs: The Medical Material Call
Medical device stamping is a materials decision before it is a die decision. SUS301 work-hardens into the spring temper that instrument hinges and contact fingers need; SUS304 covers general instrument bodies; SUS316L answers the chloride and sterilization exposure that 304 will not. For current-carrying contacts, C17200 beryllium copper holds spring force at low insertion force, and C5191 phosphor bronze is the cost-down when conductivity requirements allow. Thickness runs 0.05-3.0 mm on 21 presses, and the dimension that actually decides medical acceptance is edge quality: burr height on a 0.1 mm stainless part is a cleanliness risk inside the device, so every lot is checked on optical measurement against a defined burr spec, not just the dimensional print. Full batch traceability back to the coil, with material certificates on every shipment.
- SUS301 spring, SUS304 structural, SUS316L corrosion-critical grades
- C17200 beryllium copper and C5191 phosphor bronze for contacts
- Burr-height control verified on optical measurement per lot
- 0.05-3.0 mm coil stamping with lot traceability to the mill certificate
INSIDE THE PLANT
Inside Our Medical Stamping Line
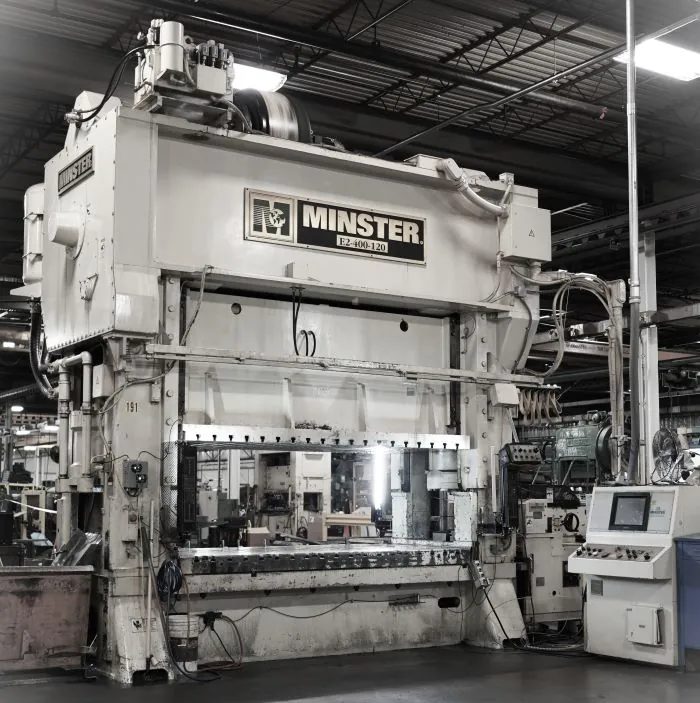
Real equipment and inspection floor from our Dongguan plant — 25–110T high-speed presses, in-house tool room, and a CMM lab running first-article inspection on every program.
MATERIALS & COMPLIANCE
Materials for Medical Applications
Material certifications and compliance documents available on every lot.
Brass
Common Alloys
Finishing
Copper
Common Alloys
Finishing
Phosphor Bronze
Common Alloys
Finishing
Stamping on Your Alloy or Coating?
Send the grade, gauge and part drawing — we confirm stampability, die and feed design, and quote on 25–110T presses at ±0.005 mm.
MTC / CoC / RoHS available per lot
DFM & ENGINEERING SUPPORT
Design for Manufacturability for Medical
We review material, tolerance, bend and volume economics before tooling starts.
What We Review
Medical device components geometry
Feature walk-through — material formability, bend radii, tolerance stack-up and plating compatibility for this part.
Sensor parts geometry
Forming checks — springback take-up built into the die, minimum bend radius on the chosen temper, hole-to-edge distances held above tear-out limits.
Surgical and orthopedic instrument components geometry
Production checks — strip pitch and coil-set discipline on the feeder, in-die sensing on critical features, burr height under 0.05 mm at press speed.
Implantable device parts geometry
Assembly checks — mating-side datum features picked with the customer, flatness and coplanarity targets set for downstream automated assembly.
What Our DFM Review Checks
Bend radii
Inside radius held at R≥1.0t on spring tempers; tighter bends flagged for anneal or grade change before die design starts.
Holes & cutouts
Hole diameter ≥0.8t, pushed to 0.6t only with hardened punch steel; thin-gauge cutouts checked for tear-out.
Burr & edge quality
Burr height held under 0.05 mm so parts mate flat in assembly and plating adheres at the edges.
Tolerance & plating impact
Critical features piloted to ±0.005 mm; plating thickness (gold 2-8 µm, tin/zinc 5-12 µm) compensated in die design.
Get a Free DFM Review
Send your drawing — receive engineering feasibility feedback, with pricing to follow.
STEP / IGES / X_T / DWG / PDF
QUALITY ASSURANCE & INSPECTION
IATF 16949:2016 Certified, Verified on Every Lot
CMM, optical measurement and 100% dimensional inspection at press speed.
 Inspection Hardware
In-House Quality Lab
- CMM & optical measurement for flat and 3D parts
- In-line vision systems inspecting at press speed
- SPC on critical features to catch drift as a trend
 Quality Standards
IATF 16949:2016 Certified
- IATF 16949:2016 automotive quality management
- ISO 14001:2015 environmental management
- PPAP documentation for automotive & EV programs
 Traceability
Full Lot Traceability
- First-article inspection against the drawing
- Lot-level material traceability back to the coil
- Inspection records on every shipment
Talk to Our Engineers About Quality Documentation
Tell us what your project requires, and our team confirms which inspection and material documentation can be included with your quote.
In-House Tool Room
Made in Our Own Tool Room
Every progressive die behind our stamped parts is 100% in-house stamping tooling — design, machining, assembly and T1 trial all under our roof. That is why tooling issues get solved on the shop floor in hours, not by email exchange with an outside die shop.
±0.001 mm Achieved
Combined machining accuracy down to ±0.001 mm, Ra0.05 µm surfaces and Ø0.05 mm micro end mills for tight die features.
30 In-House Machines
30 die-making machines — wire EDM, CNC and precision grinding — keep every die build and repair on our own schedule.
2–5 Weeks for Stamp Dies
Typical stamping die delivery in 2–5 weeks, with T1 trials run on our own presses before you commit to volume.
One Accountable Chain
Self-designed progressive dies, machined in-house, run at 60–300 SPM with CCD inline inspection — no outsourced-die handoff where quality falls between suppliers.
CASE STUDIES
Medical Case Studies
Oct 20 · 1 min read
20 Million Thin Steel Diaphragm Discs for Disposable Medical Pumps
An IV-set maker runs a flow-through valve with a pulsating pump. Inside sits a stamped steel disc that rides against the pump; because the whole…
Aug 28 · 7 min read
EV Busbar Case Study: Battery Pack Interconnects
High-volume busbar stamping for EV battery pack interconnects — tolerance, plating and delivery evidence.
Aug 28 · 7 min read
Progressive Die Case Study: Automotive Terminal Program
A multi-million-piece terminal program run on progressive dies with SPC and PPAP evidence.
ORDERING & FAQ
How to Order Medical Stampings & Frequently Asked Questions
From drawing to delivered parts: a four-step path with engineering review at the front and 100% dimensional inspection at the back — then the questions buyers ask us most.
Step 1
Submit CAD & Specs
Send 2D/3D drawings (STEP, DWG, PDF) with quantity, material, and tolerance requirements.
Step 2
DFM Feedback & Quotation
Our engineering team conducts DFM analysis and follows up with a competitive quote after the review.
Step 3
Precision Manufacturing
High-speed progressive die stamping, secondary forming, finishing, and surface treatment per your specifications.
Step 4
100% QC & Express Shipping
100% dimensional inspection, anti-corrosion packaging, and global express delivery.
What is the MOQ for Medical metal stampings?
We support prototyping from 1 piece and mass production from roughly 100k pieces upward, depending on tooling economics.
How do you guarantee material authenticity and quality documentation?
Every batch comes with material certificates and inspection reports. Heat treatment and plating logs are provided upon request.
What packaging and anti-corrosion protection do you apply for international shipping?
All finished medical metal stampings undergo ultrasonic cleaning, anti-rust treatment, individual protective sealing, and padded shockproof box packaging.
Can you stamp non-standard custom shapes or complex geometries?
Yes! We specialize in complex medical metal stampings including deep-drawn forms, multi-bend geometries, micro features, and tight-tolerance profiles per CAD specs.
Ready to Start Your Precision Stamping Program?
Send your drawing today — engineering runs a free DFM review and detailed pricing follows the review.
100% Confidential | NDA Protected | 24H Response
WHERE TO NEXT
See What Else We Stamp
Same ±0.005 mm discipline, different parts. Pick the market closest to yours and see what we run there.
Military & Defense
Meet defense programs with documented material certs and process controls, lot after lot.
Explore Industry
Solar
Deploy busbars and brackets that survive salt spray, humidity and thermal cycling.
Explore Industry
Structural Building Components
Get framing connectors and brackets that mate first time — hole patterns die-held.
Explore Industry